In-House Secondary
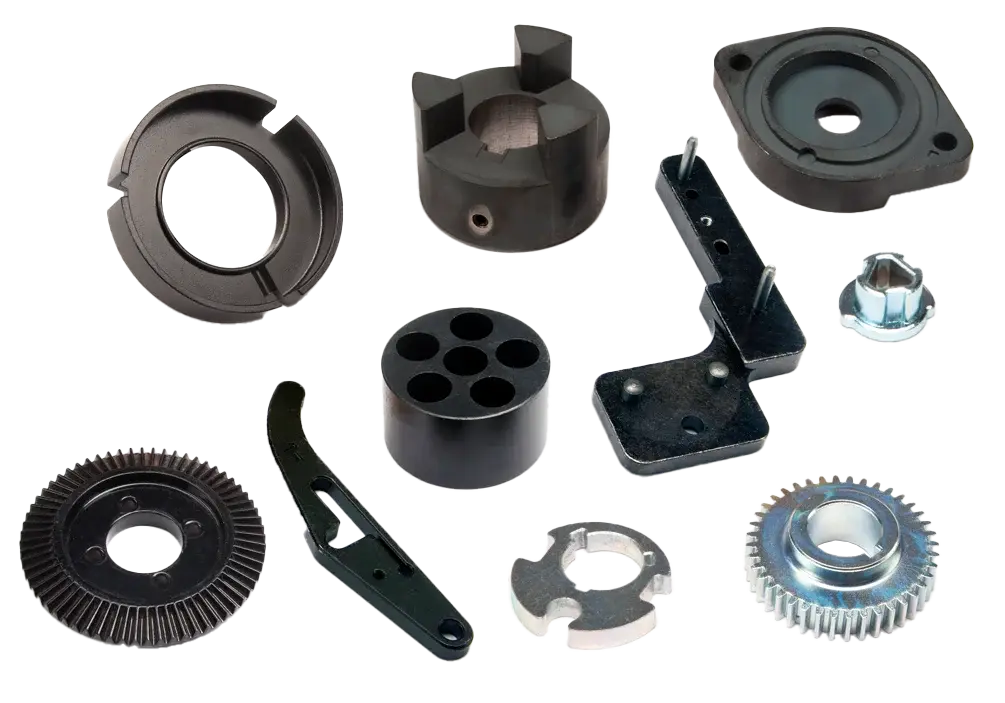
To fully accommodate its customers, Symmco knows that they may need additional operations for its component parts and even complete assemblies.
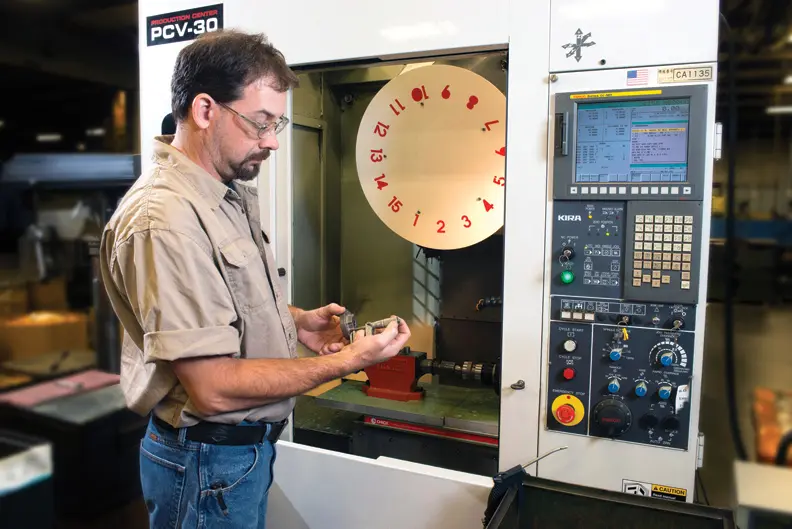
To accomplish that end, here are some of their in-house secondaries:
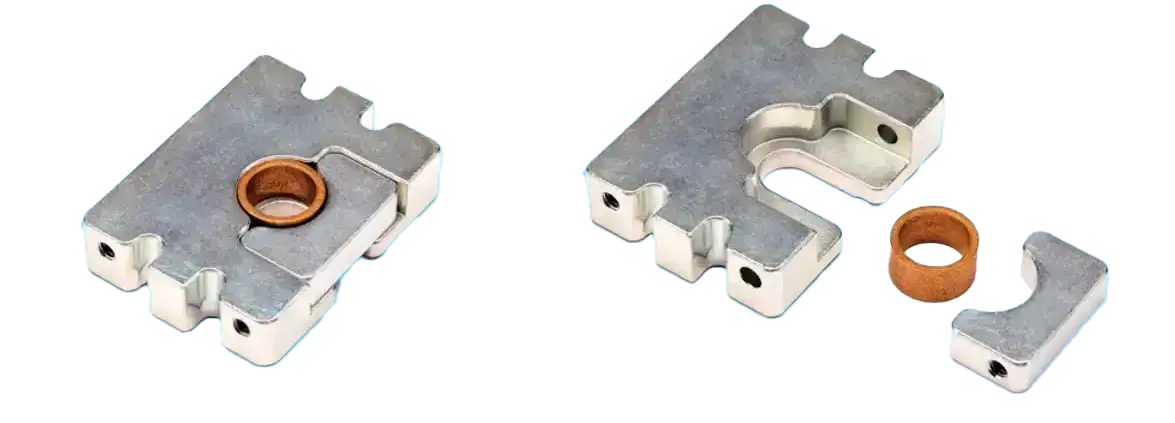
- Assembly Solutions (including the insertion of bushings, screws and shaft pins)
- Staking
- Drilling
- Tapping
- Turning
- Milling
- CNC Machining (including the use of CAD/CAM software for programing CNC equipment)
- Boring
- Vibratory Deburring (Dry or Wet Media)
- Vacuum Impregnation (including a wide range of specialty oils)
- Rotary transfers for high volume parts
Machining on lathes and mills
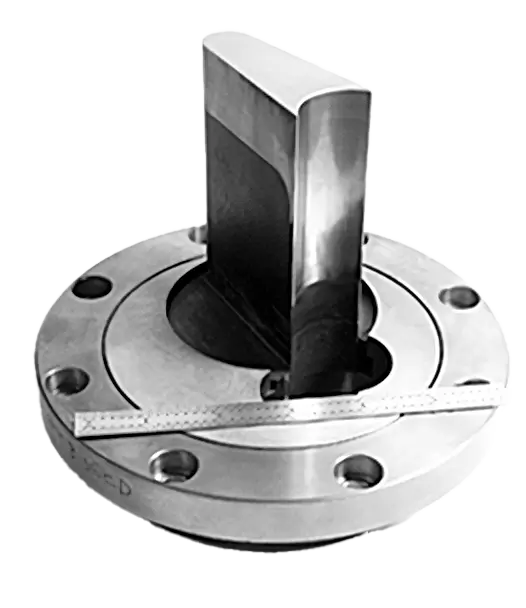
A pressed and sintered part comes out of the furnace close to its finished shape, but a drawing often carries a feature the die cannot form, and those are the operations Symmco keeps in-house. On its own lathes and mills the company drills, taps and countersinks holes, turns outside and inside diameters, hones, roller burnishes and cuts cross holes, so a part that needs a threaded hole or a finished diameter after sintering does not have to leave the plant to get it.
Where the requirement is dimensional rather than a cut feature, sizing and coining hold tolerances as tight as 0.001" without machining at all, and the Sizing + Coining page covers when that is the better route.
In-house machining
- Drilling
- Tapping
- Countersinks
- Turning outside and inside diameters
- Honing
- Roller burnishing
- Cross holes
Finishing, oil impregnation and packaging
Finishing is also done under Symmco's own roof. Parts are deburred and cleaned by dry tumbling, by media tumbling with a choice of media types, or by wet tumbling, depending on the edge and surface the drawing asks for, and the Tennessee plant adds a grit blaster for parts that need a blasted finish. A rust-preventive dip protects parts before they ship, and bearings are vacuum oil-impregnated in-house rather than sent out.
The standard impregnating oil is a high-grade, 100-viscosity, non-detergent rust and oxidation inhibited turbine oil with an effective operating range of -10°F to 200°F, and multiple oil types are available, including special military-grade oils, when an application calls for something other than the standard.
Assembly and specialty packaging close out the process, so a customer who needs a bushing pressed into a mating part, or parts packed to a particular specification, receives them that way from Symmco rather than adding a step on their own floor.
In-house finishing
- Dry tumble
- Media tumble, with multiple media types
- Wet tumble
- Rust-preventive dip
- Oil impregnation
- Assembly
- Specialty packaging
- Grit blasting, at the Tennessee plant
Which operations go to outside partners
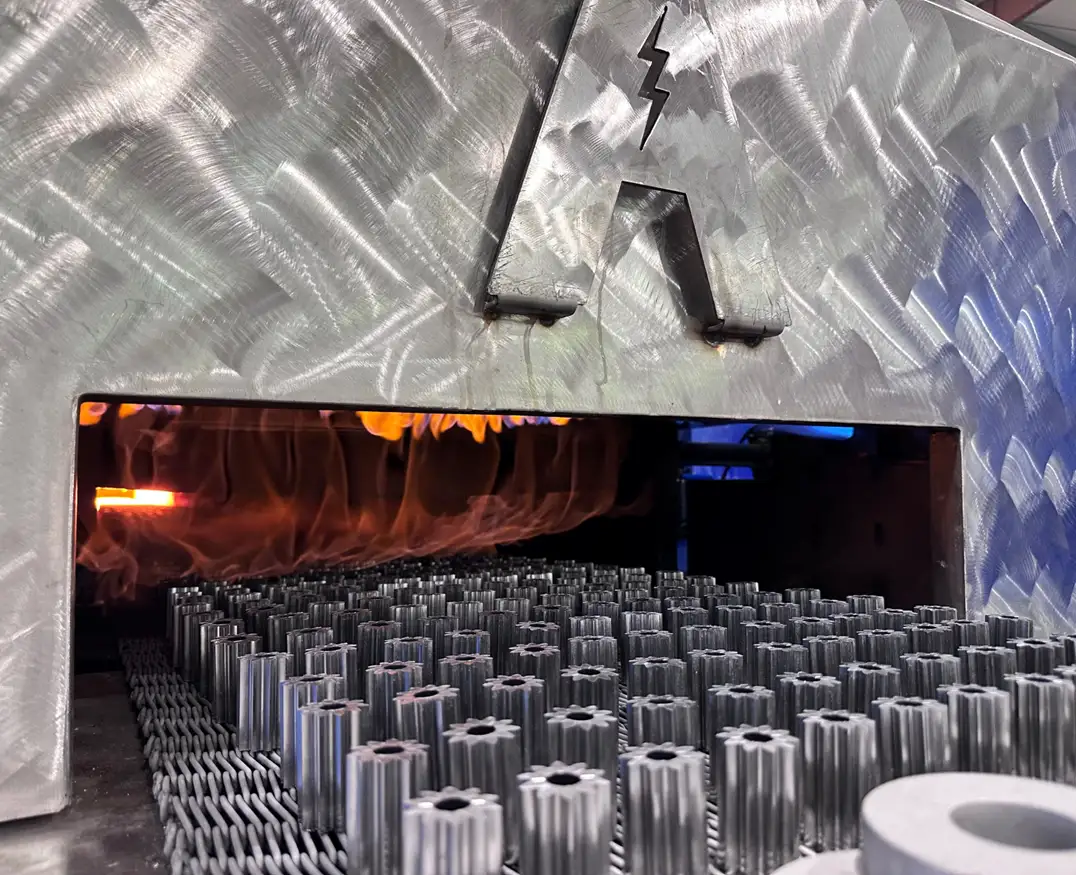
Not everything on a drawing is done under Symmco's roof: steam treating, heat treating, plating, surface grinding and resin impregnation go to outside partners that Symmco manages and coordinates, and the part still ships to the customer from Symmco as one finished piece. The Outside Secondary page describes how that is handled.
Explore Our Full Range of Capabilities
Click on one to learn more